The Definitive Engineering Guide to
FIBC Big Bag Selection.
Selecting an industrial bulk bag goes far beyond picking a fabric weight. We break down the exact mathematical and physical relationships between material density, filling automation, structural stability, electrostatic zoning, and certified cyclic safety factors.
- SWL vs SF vs GSM Decoupled
- 4 Body Structures Compared
- Type A/B/C/D Static Matrix
- Automated Line Inflow Sizing
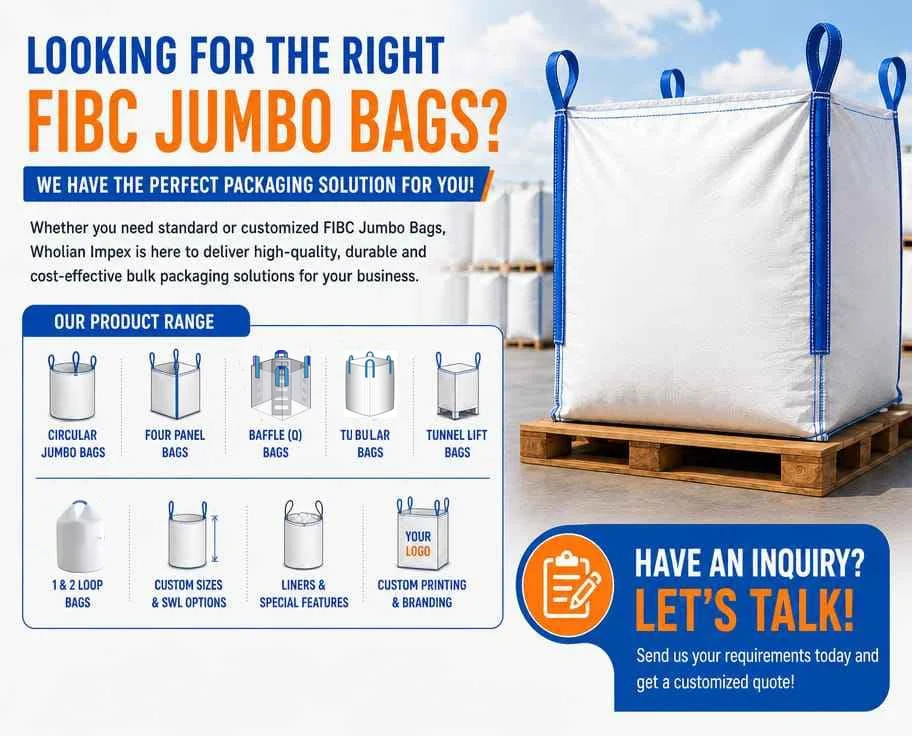
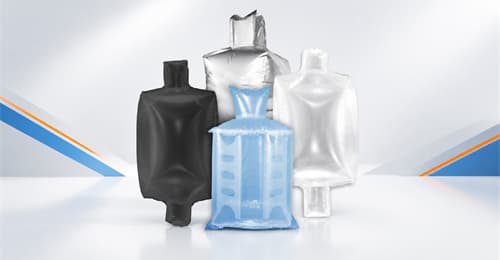
Tubular, U-Panel, Circular, and Internal Form Baffle Bags
Verified cyclic test endurance prior to final 5:1/6:1 burst test
No uncertified scrap or recycled blend in primary load fabrics
Compliant with EFIBCA, ISO 21898, US DOT, and UNECE UN rules
Interactive Decision Logic
Select Your FIBC Configuration.
Click your material characteristics, handling rig, and transport conditions below. The engine dynamically computes the exact body geometry, fabric GSM, barrier liner, and seam construction.
Material State & Flowability
Target Safe Working Load (SWL)
Filling Line Inflow System
Storage & Logistics Requirement
Recommended Bag Model
Geometric Anatomy
Four Core Body Structures.
The bag structure determines how hydrostatic bulk pressure distributes across seams and corners during lifting and long-distance container transit.
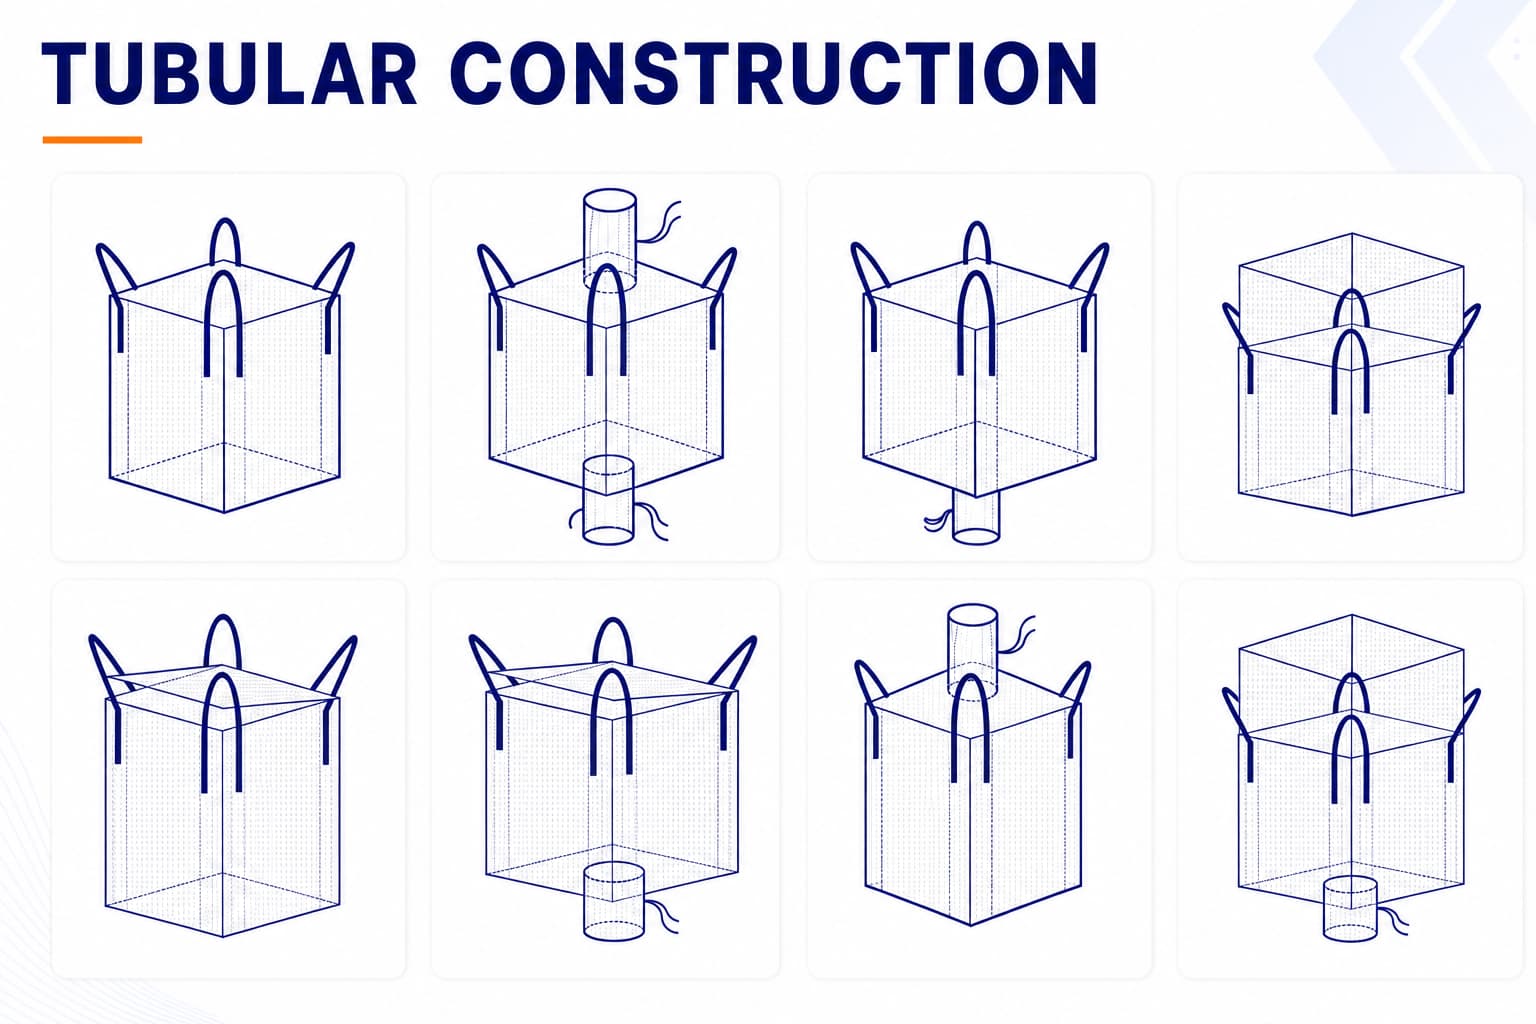
Tubular Body with Two Vertical Seams
The body is folded from flat-woven polypropylene fabric and sewn into a tube with two vertical seams. As the economical general-purpose workhorse, it keeps a predictable rectangular footprint and suits the widest range of dry bulk solids.
Key Advantages
- Economical, fast and widely available construction
- Keeps a squarer footprint than a circular seamless body
- Balanced all-round performance for general dry bulk loads
Limitations
- Two vertical seams need sift-proof cords for fine powders
- Moderate bulging under heavy hydrostatic pressure
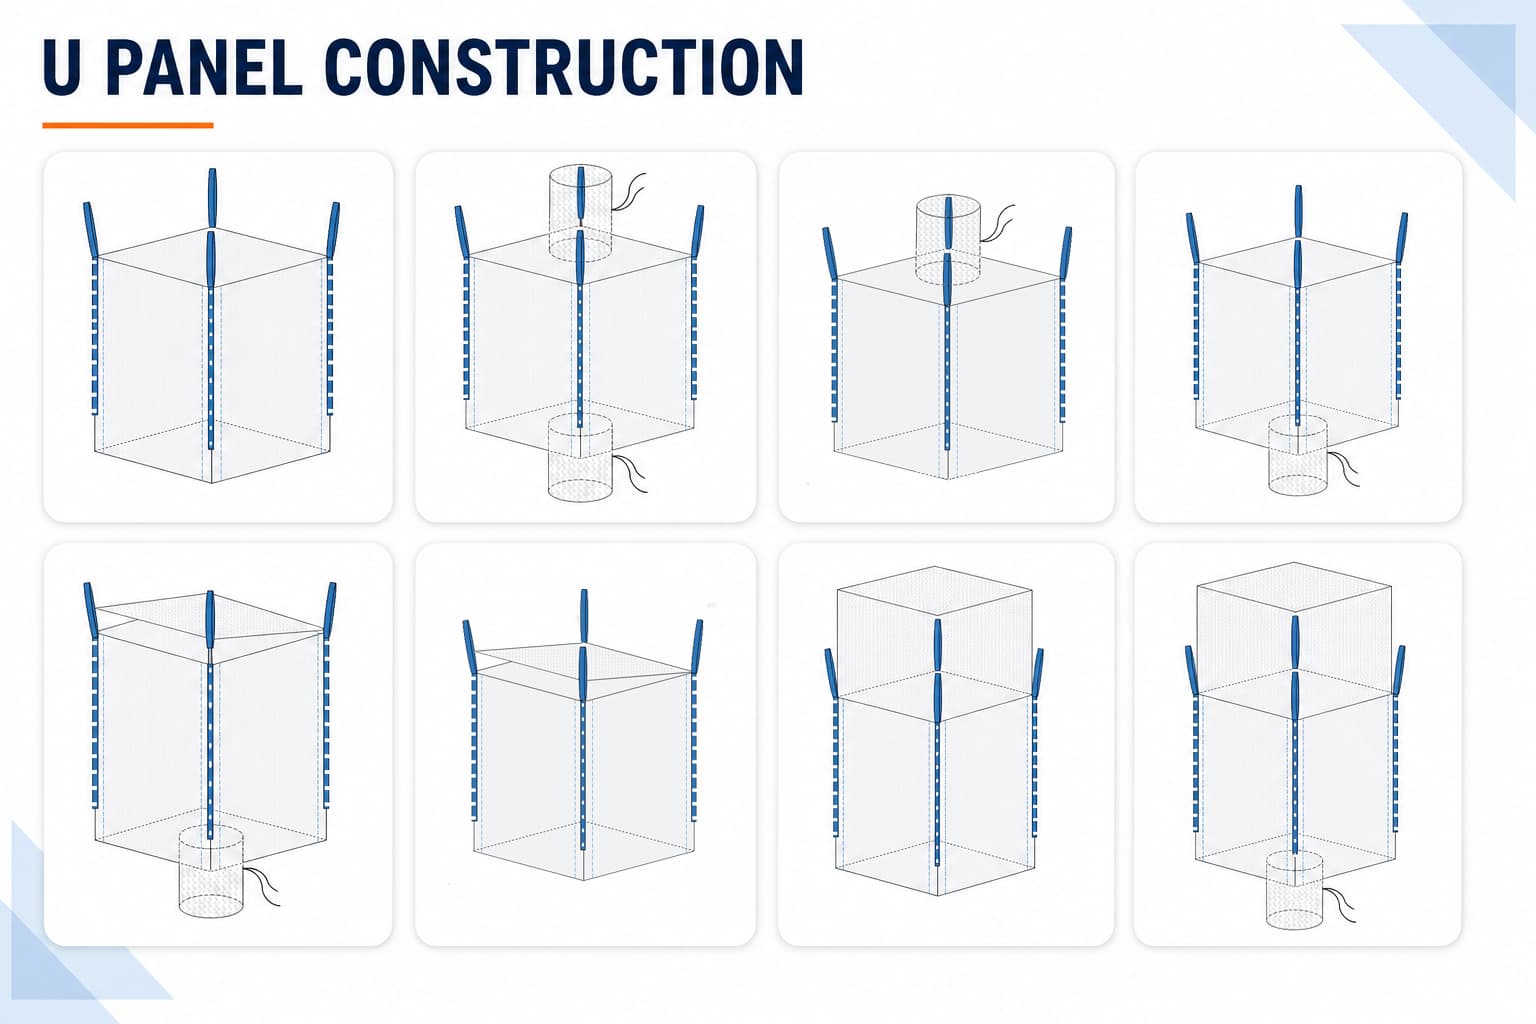
U-Panel Structural Integrity
Consists of one continuous fabric piece forming the bottom and two opposite sides, plus two sewn side panels. This standard global design delivers tremendous lifting equilibrium and dynamic load distribution.
Key Advantages
- Continuous bottom base prevents bottom seam tears
- Maintains square shape better than circular bags
- Excellent balance of high SWL load bearing and cost
Limitations
- Has vertical side seams requiring sift-proof cords for powder
- Moderate bulging under heavy hydrostatic pressure
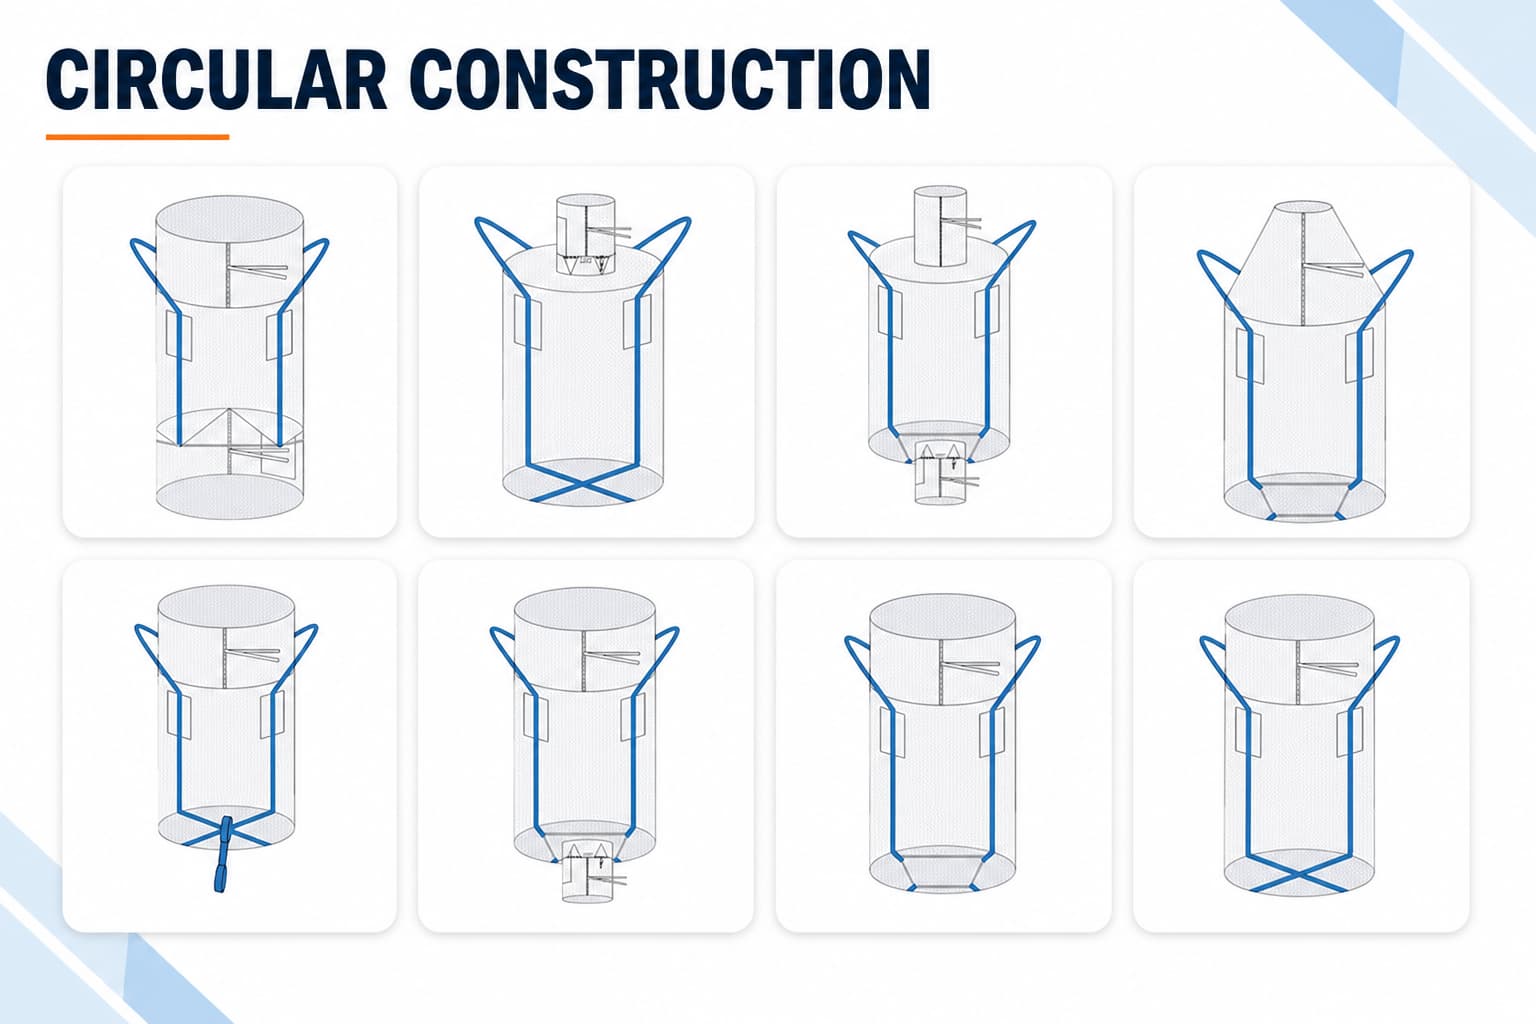
Circular Seamless Body
Woven directly on circular looms without vertical side seams. The body is an unbroken cylinder sewn only at the top and bottom assemblies, minimizing potential leakage avenues for fine powders and flowing solids.
Key Advantages
- Zero vertical side seams eliminate sift vulnerabilities
- Cost-effective, high-volume automated production
- Ideal for high-fluidity powders and fine chemicals
Limitations
- Naturally rounds out and bulges when filled
- Lower space efficiency in ocean containers vs Baffle bags
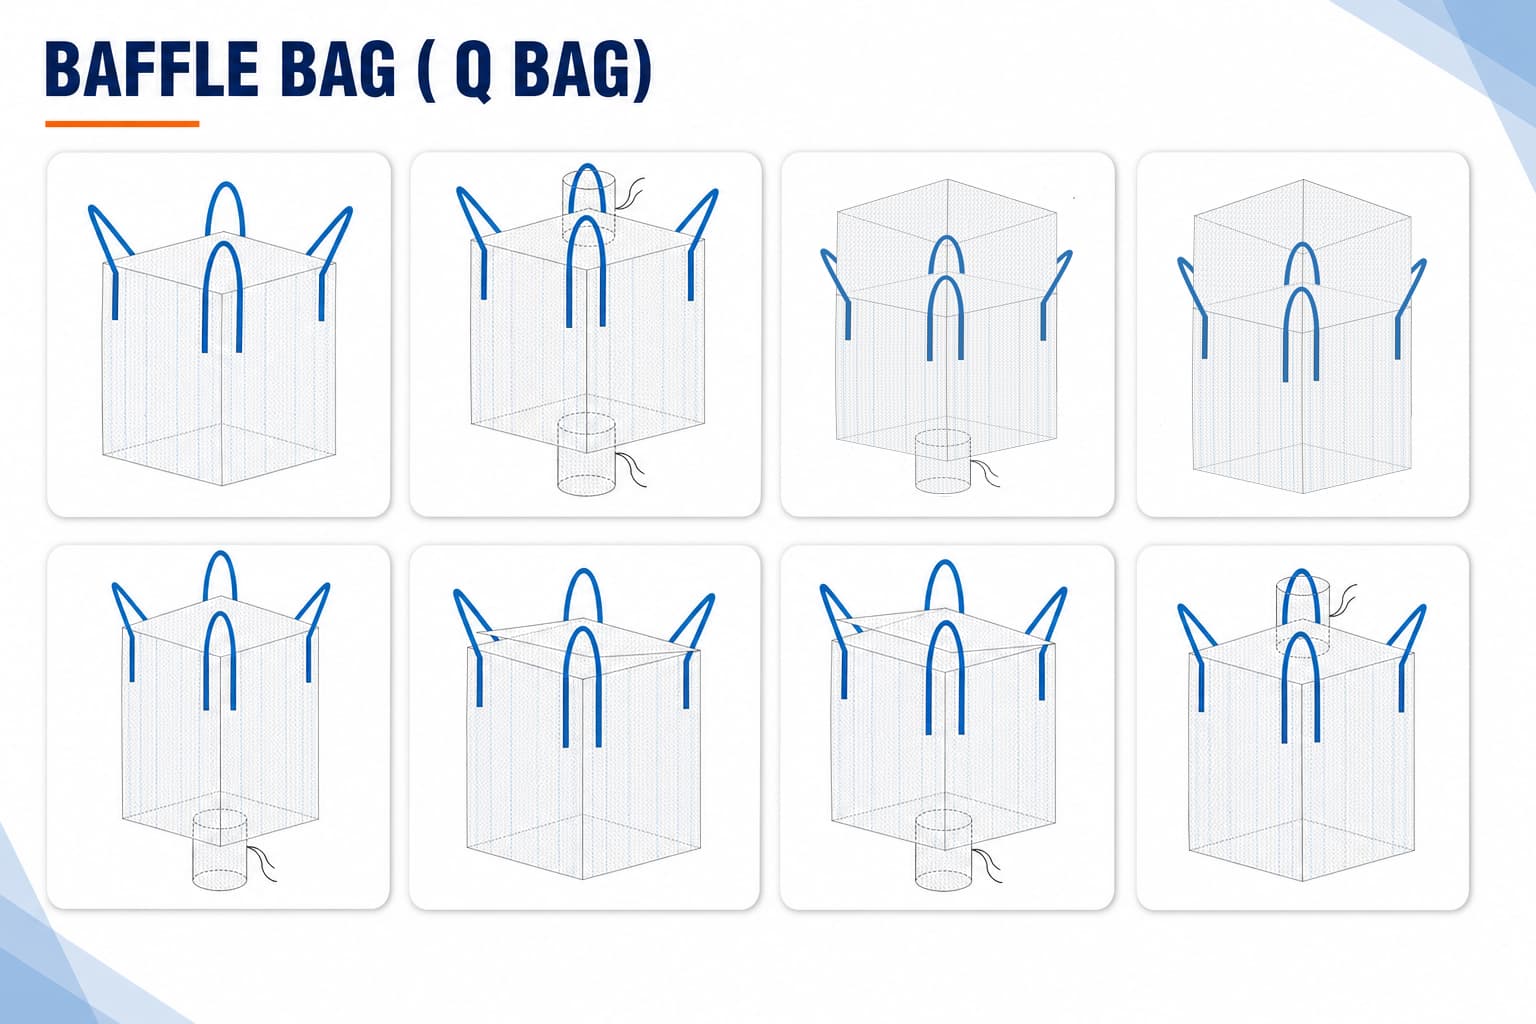
Baffle Bag (Form-Stable Q-Bag)
Internal fabric baffles with flow perforations sewn across the four corners. The baffles prevent outward rounding, ensuring the big bag retains a rigid square footprint even when completely filled with heavy solids.
Key Advantages
- Increases ocean container shipping volume fill by up to 25%
- Enables stable 2-high or 3-high warehouse stacking
- Eliminates pallet overhang and forklift punctures
Limitations
- Higher manufacturing complexity and unit production cost
- Requires dry free-flowing materials to pass corner perforations
Modular Customization
Top, Bottom & Lifting Rigs.
The interface between your filling station and discharge hopper dictates operator safety and throughput speed. Configure each module to your equipment specs.
Filling Top Configurations
Engineered to seal tightly over plant filling pipes, eliminate airborne dust escapes, and protect cargo against moisture ingress.
- Spout Top: Standard Ø35-50cm cylinder with web tie-off.
- Duffle Top: Full-width skirt for wide automated chutes.
- Open Top: Hemmed opening for manual loading and scrap.
- Conical Top: Funnels high-angle powders for maximum volume.
Discharge Bottom Systems
Facilitates controlled, zero-spill material emptying while ensuring complete operator safety during suspension.
- Spout with Petal: Protective star iris covering bottom nozzle.
- Full Drop Bottom: Base unlatches instantly for sticky sludge/cake.
- Plain Flat Base: Solid bottom for slit-and-dump single trip use.
- Remote Rip-Cord: OSHA-safe untying from outside danger zone.
Lifting Loops & Webbing
High-tenacity polypropylene webbing woven in-house. Certified against cyclic fatigue and fork abrasion.
- Cross-Corner: Arched loops stay open for rapid forklift entry.
- Side-Seam: Sewn into vertical seams; high tensile strength.
- Stevedore Straps: Interconnected loops for single-crane lifts.
- Tunnel Sleeves: Continuous fabric tunnels for direct tine insertion.
Barrier Science
Fabric & Liner Barrier Selection.
Matching the right fabric permeability and barrier layer prevents moisture damage, oxidation, powder dusting, and condensation during long-distance multimodal transport.
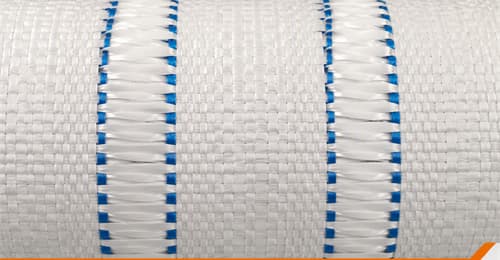
Uncoated (Breathable) Woven PP
The raw polypropylene woven fabric allows natural air permeability. Essential for agricultural produce, coffee beans, firewood, and minerals that release moisture and require ventilation to prevent mold.
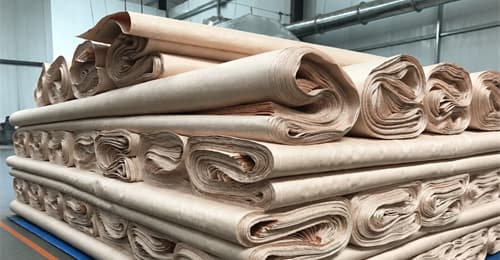
Extrusion Coated (Laminated) Fabric
A thin, molten layer of polypropylene/polyethylene (20-30 GSM) is thermally laminated onto the woven fabric, sealing the microscopic gaps between yarns against fine dust leaks and external moisture splash.
Polyethylene & Barrier Liners
Inserted independently or glued to the outer bag walls. Options include gusseted PE tubes, form-fit bottle shape liners, EVOH oxygen barriers, and aluminum foil for total atmospheric isolation.
Engineering Science
SWL, SF & GSM Decoupled.
A high fabric GSM does not automatically guarantee load safety, and a 5:1 Safety Factor does NOT mean the bag can hold five times its rating in daily operations. Click each parameter to understand the physical relationship.
SWL (Safe Working Load)
The legal declared maximum payload capacity (e.g. 1,000 kg / 2,000 kg)SF (Safety Factor: 5:1 / 6:1)
Destructive test margin under ISO 21898 cyclic rig protocolsGSM (Grams Per Square Meter)
Fabric weight measurement; represents material consumption, not total strengthSWL (Safe Working Load): Maximum Operational Limit
SWL represents the certified maximum payload weight that an FIBC is designed and rated to safely carry during ordinary lifting, shipping, and storage. It is illegal and dangerous to intentionally exceed the stated SWL regardless of safety factor.
Engineering Fact: SWL is the operational ceiling (e.g. 1,000 kg). Exceeding SWL invalidates insurance, tests, and standard factory liability.
Safety & Regulatory Standards
Risk, Environmental & Compliance Matrix.
Operating in hazardous dust environments, open sunlit wharves, or food cleanrooms requires explicit certified configurations. Filter the matrix below by compliance category.
Type A & B Standard Bags
IEC 61340-4-4Type A has no electrostatic protection; suitable only for non-flammable bulk goods. Type B fabric possesses breakdown voltage <6kV, preventing propagating brush discharges with MIE >3mJ.
Type C Groundable Conductive FIBC
Active GroundingFeatures interconnected carbon/conductive grid threads sewn into fabric and loops. Must be physically grounded to earth during filling and discharge (resistance to ground <10^8 Ω).
Type D Static Dissipative FIBC
Passive DissipationConstructed with quasi-conductive fibers (e.g. Crohmiq) that safely dissipate charge into the surrounding air via low-energy corona discharge without requiring grounding cables.
High UV Outdoor Weathering
> 200 KLy TestedStandard PP degrades rapidly under solar ultraviolet radiation. We compound hindered amine light stabilizers (HALS) masterbatch (1.5% to 3.0%) into the extrusion melt to preserve yarn tensile strength.
UN Certified Dangerous Goods
UNECE Orange BookUN codes (13H1 to 13H4) represent design-type test certification for specific chemical classes. Requires mandatory drop tests, topple tests, righting tests, tear propagation, and stacking tests.
Food & Cleanroom Hygiene
FDA & EU 10/2011Manufactured exclusively from certified virgin PP resin without recycled content or toxic plasticizers. Fabric edges are ultrasonic heat-sealed to eliminate loose fiber fraying.
Factory Governance Protocol
Specification Confirmation Checklist Before Production
To protect both buyer and manufacturer, no custom FIBC enters mass circular weaving without mutually signing off on these exact tolerance and quality benchmarks.
1. Dimensional & Mass Tolerances
- Height, width, and base dimensions verified to ±15mm tolerance.
- Base fabric GSM verified to ±5% across full roll width.
- Inflow/outflow spout length and diameter matched to plant flange.
2. Seam & Sift-Proof Inspection
- Stitch density locked at 10-12 stitches per 10cm run.
- Non-woven felt cord placement verified on all vertical seams.
- Chainstitch lock tail secured to prevent seam unraveling.
3. Rig Testing & Golden Sample
- 70-cycle top lift test executed on pre-production sample.
- Destructive burst test confirms required 5:1 or 6:1 ratio.
- Sealed Golden Sample versioned and archived for QA audits.
Direct Factory Consultation
Still Unsure Which FIBC Matches Your Line?
Send us your bulk solid material data sheet (MSDS), filling chute diameter, and target packaging budget. Our engineering leads will provide complete technical CAD drawings and material recommendations within 24 hours.